
Choosing the Right Fabric Surface Tension for Digital Printing

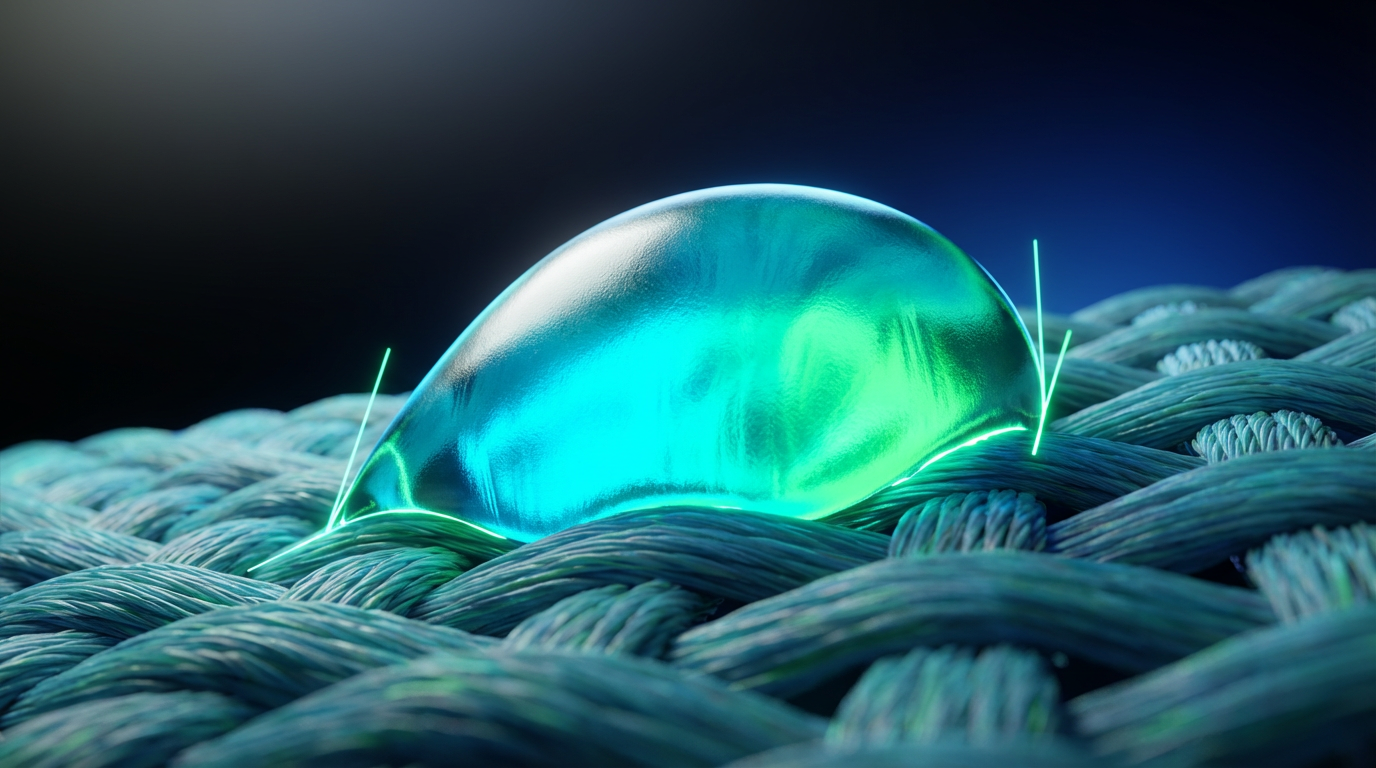
Table of Contents
- Surface Tension, Surface Energy, and Wettability: The Real Basics
- How Fabric Construction Changes Wetting, Adhesion, and Print Quality
- Fibers for Performance Printing: Polyester, Nylon, Cotton, and Blends
- Coatings, Pretreatments, and Engineered Fabrics for UV, Latex, and Pigment Inks
- What Surface-Tension Mismatch Looks Like on Real Gear
- Environmental Control: Temperature, Humidity, and Dimensional Stability
- Application-Driven Choices: Jerseys, Shells, Banners, and Soft Gear
- A Practical Workflow for Dialing In Surface Tension on Sports and Adventure Fabrics
- Quick Answers to Common Questions
- Is there a single “ideal” surface tension number for digital printing on fabric?
- How do water‑repellent or stain‑resistant finishes affect digital printing?
- Can I use the same surface tension setup for both jerseys and outdoor banners?
- References
When you hammer a downhill trail, lean into a track-day corner, or throw a roost on a motocross course, your gear is doing more than protecting you. It is carrying your colors, your sponsors, and your story. As someone who spends a lot of time around Kawasaki sportswear, soft signage, and outdoor adventure setups, I can tell you this: the difference between a print that screams “race ready” and one that looks flat and tired often comes down to one invisible factor.
Surface tension.
Get ink surface tension and fabric surface energy wrong, and your bold graphics bead, bleed, or crack. Get them right, and your jerseys, tension-fabric backdrops, and outdoor banners stay sharp, bright, and bonded through rain, UV, mud, and repeated washes. This guide walks through how to think about “fabric surface tension” for digital printing in the real world of high-performance sports and adventure gear, grounded in lab research and production know-how from sources like Luminite, Dropletlab, Textiles.org, Digital Output, and super‑wide specialists such as Amayse.
Surface Tension, Surface Energy, and Wettability: The Real Basics
In printing and coatings, people often say “fabric surface tension.” Technically, surface tension belongs to liquids, while solids like fabrics have surface energy. What actually matters is how those two interact.
Surface tension, as flexographic experts at Luminite explain, is a property of the ink. It describes how strongly the liquid’s molecules pull together at the surface, and it is measured in dynes per centimeter. High surface tension makes droplets want to stay round and tight. Low surface tension lets them spread out more easily.
Surface energy is the solid-side equivalent. For textiles and coatings, Dropletlab describes it as the extra energy sitting at the fabric’s surface compared with its interior. A high‑energy surface tends to attract liquids; a low‑energy surface tends to repel them. That is why a durable water‑repellent shell makes raindrops bead, while a raw cotton tee soaks them up.
Wettability is the result of this matchup. If the ink’s surface tension is too high for the fabric’s surface energy, the ink beads and refuses to cover. If the ink’s surface tension is tuned lower than the fabric’s surface energy, it wets the fibers, forms a continuous film, and can bond properly. Luminite notes that, in a printing system, you want surface tension and surface energy to gradually step up from ink to image carrier to final substrate so each step pulls the ink cleanly along.
Dropletlab goes one level deeper with contact angle: the angle between a droplet and the surface. A low contact angle means the drop spreads and wets well, while a high contact angle means poor wetting. In production, people measure this with goniometry, but you see the same thing in the shop when you drip water or test ink on a swatch and watch whether it spreads evenly or beads instantly.

There is also static versus dynamic surface tension. Static values describe equilibrium; dynamic values describe what happens over time as surfactants, solvents, and temperature changes kick in. For fast inkjet droplets hitting a fast‑moving sports banner fabric, dynamic behavior matters a lot. Dropletlab points out that dynamic surface tension is critical whenever interfaces change quickly, which is exactly what happens when microscopic ink drops hit a coated polyester knit at speed and immediately start to level, wick, and dry.
How Fabric Construction Changes Wetting, Adhesion, and Print Quality
Once you understand that printing is a surface-tension tug‑of‑war, the next question is obvious: what does the fabric itself do to that balance?
Research in Fashion and Textiles on 3D‑printed composite fabrics shows that surface roughness, porosity, fabric density, and structure dramatically affect peel strength, which is a direct measure of how well a polymer layer sticks to a textile. Using non‑contact microscopy and X‑ray tomography, the study found that:
The roughness parameter Ra had a very strong correlation with peel strength, with a Pearson coefficient around 0.92, while a larger‑scale waviness parameter was weaker. In simple terms, the micro‑texture of the fibers matters more than big, gentle ripples.
Highly porous and rough nonwoven and spun fabrics delivered the highest peel strength, with one nonwoven reaching about 39.6 percent porosity and showing the strongest adhesion. That extra pore volume lets molten material penetrate and mechanically lock into the structure.
Fabrics with high warp and weft density had lower porosity and lower peel strength. They were smoother, less open, and left less space for polymer to flow and grab.
Although that study focused on 3D‑printed polymers rather than liquid ink, the physics are the same. When you print a thick latex film on an outdoor cushion or build up UV layers for a backlit SEG frame, you want enough surface roughness and accessible pore space for the ink film to grip, not just sit like a fragile skin on top.
A second study published in MDPI examined how different weaves, all made from the same yarn, changed surface topography and print behavior. Plain, twill, and atlas weaves created distinct roughness and texture, even at the same yarn count. Microscopy revealed that ink droplets lost their circularity, became star‑shaped, and tended to pool in inter‑yarn gaps while leaving yarn tops more lightly covered. Color measurements confirmed that these structural differences pushed prints lighter or darker and more or less saturated, even when ink and design stayed constant.
Two practical lessons fall straight out of this research for sports and outdoor printing. First, you cannot just say “polyester” or “cotton” and be done. A smooth filament polyester plain weave behaves nothing like a fuzzy spun polyester nonwoven when ink hits it. Second, the rougher, more open constructions that give you stretch and breathability also change how ink spreads and locks in. You have to balance comfort, performance, and print behavior.


Fibers for Performance Printing: Polyester, Nylon, Cotton, and Blends
For Kawasaki‑style gear, the usual suspects are polyester, nylon, and various blends. Cotton shows up in lifestyle tees and casual hoodies, while polyester and nylon dominate technical sportswear, shells, and soft signage.
Guides from NB Printex, RFP Design, and GZ Henry all point to polyester as the dominant fabric for digital printing when you want high color vibrancy, fast drying, and serious durability. With dye‑sublimation or disperse inks, the dyes literally migrate into the polyester and lock into the polymer matrix under heat. That is why your sublimated race jersey can handle repeated washing and UV exposure without the design peeling off.
Nylon plays a slightly different role. It offers high abrasion resistance and quick drying, which is why it is popular in activewear and outdoor gear. Digital printing usually uses acid or disperse inks on nylon, often with pretreatment to improve adhesion, as noted in both textile printing guides and the MDPI weave study. Nylon’s surface chemistry includes functional groups that can interact strongly with certain polymers, which is great for adhesion but still sensitive to surface contaminants.
Cotton brings comfort and breathability, especially for everyday apparel and lifestyle pieces, and it works well with reactive and pigment inks. However, as GZ Henry and other fabric‑selection guides point out, prints on cotton are typically less vibrant than on polyester and can be more prone to fading and shrinkage unless you lean heavily on pretreatment and post‑treatment. In the 3D‑printed composite study, cotton actually showed the lowest peel strength among the tested fiber types, largely because unscoured cotton still carried processing oils that made the surface more hydrophobic. That is a powerful reminder: what is on the fabric surface right now matters more than the fiber’s ideal textbook chemistry.
Blends, such as poly–cotton or nylon–spandex, are everywhere in performance gear. They combine comfort, stretch, and durability, but they complicate printing because each fiber type prefers a different ink chemistry. As Textiles.org emphasizes, a digital system can only run one ink chemistry at a time, so you choose the chemistry that best matches the dominant fiber and accept compromises on the others. Surface tension tuning and coating become even more critical in this blended world, because you need the ink film to wet and lock across fibers that do not all behave the same way.
Coatings, Pretreatments, and Engineered Fabrics for UV, Latex, and Pigment Inks
In adventure gear and soft signage, you cannot rely on fiber alone. Coatings and pretreatments are the unsung heroes that bring surface tension, surface energy, and ink chemistry into alignment.
Digital Output describes how modern UV‑ and latex‑optimized textiles are factory‑coated specifically to create a firm, stable surface, improve ink bonding, and prevent fabric shifting during printing. Latex‑printable fabrics often use proprietary coatings to anchor the water‑based latex film to the fabric surface, which sharpens edges, improves wash and rub resistance, and keeps the hand as soft as possible. UV‑printable fabrics can sometimes be printed without pretreatment, but coatings still help expand color gamut, reduce scratching, and control light for backlit and blackout applications.
ITAC Adhesives lays out the coating side from a surface‑science angle. In coatings, lowering liquid surface tension improves wetting and helps form a smooth, continuous film instead of pinholes or beads. They point out that surfactants and flow agents are common tools to push surface tension down into the right window for a given substrate. Temperature shifts also matter because surface tension tends to drop as liquids warm up. The message is simple: you tune surface tension by adjusting formulation, blending, and process, not just by crossing your fingers at the press.

Textiles.org adds the crucial pretreatment step for dye‑based digital systems. For most acid, reactive, and disperse dyes, the ink itself cannot carry all the chemistry needed for fixation because inkjet heads demand very low viscosity. Instead, you apply a coating to the fabric that supplies fixation chemicals and uses thickeners to limit lateral ink bleed. After printing, heat and wash‑off lock the dyes into the fibers and remove excess chemistry. Pigment ink is the outlier here, since it often relies on a binder and heat‑fusion instead of deep diffusion into the fiber. That simplifies the process but typically narrows color gamut and can stiffen the hand.
The common thread is that coatings and pretreatments are your main levers on the solid‑side of the surface tension equation. They raise or lower surface energy, change roughness, fill or leave pores, and even alter dynamic contact angles. When a coated polyester feels “perfectly printable,” it is because someone has engineered those properties so your ink surface tension sits in a sweet spot for that fabric.
What Surface-Tension Mismatch Looks Like on Real Gear
You do not need a lab tensiometer to know when surface tension is wrong. You just have to look closely at the print.
Experts in flexo and coating, including Luminite, ITAC, and Henghao, describe the same failure modes across different processes. Good wetting gives you a smooth, even film with clean edges and solid coverage. Poor wetting gives you gaps, halos, and unpredictable defects.
Here is how those issues translate to the fabrics we live with in the paddock, trailhead, or expo hall.
|
What you see on the fabric |
Likely cause |
Surface tension story |
|---|---|---|
|
Beads, islands, or “fish eyes” where ink refuses to cover |
Ink too high in surface tension for that fabric/coating |
Ink’s cohesive forces are stronger than its attraction to the substrate, so drops pull together and retract |
|
Uneven, spotty solid areas and pinholes |
Inadequate wetting or contamination on the fabric surface |
Surface energy is too low in places or contaminated, so local wetting fails |
|
Over‑spreading, blurry edges, loss of fine detail |
Ink surface tension pushed too low, or fabric too absorbent |
Drops spread too far before drying, or ink wicks deep into open pores |
|
Poor transfer from intermediate surface (plate, belt, paper) |
Wrong surface tension sequence in the ink train |
Each step does not provide higher surface energy, so ink stays behind instead of fully transferring |
|
Cracking or flaking of thick printed areas |
Weak mechanical anchoring or over‑brittle ink film |
Adhesion is dominated by a brittle film rather than a well‑wetted, interlocked interface |
If you are seeing these symptoms on polyester banners, nylon duffels, or cotton tees, you are not just fighting “bad fabric.” You are looking at a surface tension and surface energy mismatch that you can fix with better coating, different ink, or more controlled environment.
Environmental Control: Temperature, Humidity, and Dimensional Stability
Performance prints do not live in a climate‑controlled lab. They live in changing humidity, heat, dust, and mechanical stress. The way you store and handle fabrics before printing has as much impact on surface behavior as your ink settings.
Amayse, a specialist in super‑wide tension fabric systems, stresses environmental control for their textiles. They store fabrics at controlled temperature and humidity to keep behavior predictable. That stability is essential when graphics have to stretch into frames with mill‑level precision without warping logos or compromising clarity.
Dropletlab notes that contact angles and sliding behavior change with temperature, humidity, and contamination. Add a dusty warehouse or a sweaty production space to a moisture‑sensitive coating and you can easily see the same fabric print differently from one week to the next. ITAC reminds us that solvent evaporation and surface tension also shift with temperature; warming an ink too far can completely alter its wetting and drying profile.
If you are chasing consistent Kawasaki green across jerseys, pit canopies, and trackside banners, you should think like a lab tech for at least a moment. Keep roll storage reasonably dry and stable. Let fabrics acclimate before printing instead of going straight from a cold truck into a hot printer environment. Protect coated surfaces from handling and contamination. When prints suddenly change with no obvious RIP or head issue, check the room and the fabric, not just the machine.

Application-Driven Choices: Jerseys, Shells, Banners, and Soft Gear
Choosing the “right” surface tension is never abstract. It is always tied to how the printed fabric will be used, abused, and seen.
For sublimated polyester jerseys and base layers, you are usually working with inks that penetrate and lock into the fibers. Here, the big risk is ink spreading too far on open, stretchy knits and blurring small sponsor logos. Research on weave and texture shows that rougher, more complex surfaces lead to more irregular dot shapes and color shifts. You want enough pretreatment to control lateral spread while still letting dyes migrate into the fiber under heat.
For outdoor banners, inflatable arches, and SEG backdrops, UV or latex systems shine because they cure quickly and produce dense, vibrant color, especially for backlit graphics. Digital Output emphasizes that UV‑ and latex‑ready fabrics rely heavily on coatings to hold a flexible but well‑anchored ink film. Rough, porous textiles need coatings that limit deep soak‑in so the film stays at the surface and reflects light efficiently. High stretch knits that curl or distort in the feed are flagged as risky, not because they cannot be printed, but because controlling surface tension and dimensional stability together becomes much harder.
For adventure luggage, seat covers, and technical outerwear, nylon and rugged poly blends combine with coatings for water resistance, stain resistance, or self‑cleaning. Dropletlab mentions sliding angle as a metric for water‑shedding surfaces, which is great for raingear but terrible for adhesion if you want a thick, durable print. Here, you often have to selectively remove or modify finishes in the print zone or use special primers that raise local surface energy so the ink can wet and bond without compromising the overall water repellency of the gear.

The key pattern is that application drives not just fiber and construction, but also the target wetting behavior. A breathable, water‑repellent jacket wants raindrops to roll off, but your digital print still needs to wet well enough to grip. A tension frame graphic needs controlled stretch and predictable dimensions, so you choose fabrics and coatings with stable surface properties under the mechanical loads of installation.
A Practical Workflow for Dialing In Surface Tension on Sports and Adventure Fabrics
In practice, getting surface tension right is more process than magic. The teams that consistently produce pro‑level prints for high‑performance gear usually repeat a similar sequence.
First, they define the end use and durability expectations. A short‑run indoor retail display is one thing; a race jersey that will be washed, flexed, and sweat‑soaked all season is another. Research and industry guides point out that ink–fiber compatibility, wash fastness, UV resistance, and mechanical abrasion are inseparable from surface wetting and adhesion.
Second, they match ink chemistry to fiber family. Textiles.org and NB Printex summarize the standard pairings: disperse or sublimation for polyester, reactive for cotton and regenerated cellulosics, acid for nylon and for ultra‑vibrant silk or wool, pigment when you need broad fabric coverage with a simpler workflow. Systems that can handle multiple ink chemistries give you more freedom to tune surface tension for each substrate.
Third, they choose or specify the fabric and pretreatment with printing in mind. Digital Output reports that UV and latex‑optimized textiles are almost always factory‑coated to deliver stable feeding, firm surfaces, and reliable adhesion. Pretreated fabrics are also common in reactive and acid systems, where coatings are tailored to ink families. Avoiding fabrics with uncontrolled stretch, fraying edges, or unstable finishes is as much a surface tension decision as a mechanical one.
Fourth, they actually test wettability. Luminite mentions goniometry as a formal method; Henghao describes practical ink drop tests and dyne testing. In a production environment, that might mean using test fluids of known surface tension to confirm substrate surface energy, or simply laying down a controlled patch of ink and evaluating how fast and how evenly it spreads. Dropletlab encourages measuring dynamic contact angles, because those describe how wetting changes as the droplet advances and recedes, which matters for droplet trains landing in real printing.
Fifth, they adjust formulation and process. When wetting is inadequate, ITAC highlights the use of surfactants, flow agents, and compatible solvents to lower ink surface tension and improve spread. When wetting is excessive and detail is lost, you can step back on surfactants, modify pretreatment to increase surface resistance, or adjust curing and drying profiles so ink sets faster. Temperature control on ink and fabric is part of this, since surface tension is temperature‑dependent.
Finally, they validate in real‑world conditions. Digital Output notes that outdoor‑focused fabrics must stand up to water, UV, wrinkling, and heavy wear without prints cracking or getting brittle. Textile printing studies on roughness and porosity emphasize that substrates with high fuzz and open pore structure offer more pathways for mechanical locking and stronger peel strength. That is good for adhesion, but you still have to see how the final stack behaves after repeated washing, folding, and flexing.
From a rider’s or brand’s perspective, the goal of all this science is simple. You want your colors to hit hard, stay put, and feel good, whether they are wrapped around a frame in a tension system, stretched over armor on a trail, or hanging above a paddock in the sun.
Quick Answers to Common Questions
Is there a single “ideal” surface tension number for digital printing on fabric?
No. Technical sources from Luminite and ITAC are very clear that good wetting is about the relationship between ink surface tension and substrate surface energy, not one magic value. The ink usually has to sit somewhat lower than the fabric’s surface energy so it can wet and spread, but the exact gap depends on the coating, the fabric construction, and the printing method. That is why dyne testing and small‑scale trials on actual fabrics are still standard practice.
How do water‑repellent or stain‑resistant finishes affect digital printing?
Surface‑science guidance from Dropletlab and textile studies on adhesion show that hydrophobic finishes lower surface energy and raise contact angles. That is great for making raindrops or mud roll off, but it makes ink wetting and adhesion much harder. In the 3D‑printed composite fabric study, unscoured cotton with residual oils showed poorer adhesion than expected. The same thing happens when you try to print on heavily finished performance fabrics. The usual solutions are pretreatments that locally raise surface energy, cleaning or scouring steps before printing, or selecting fabrics where the print zone is engineered specifically for ink reception.
Can I use the same surface tension setup for both jerseys and outdoor banners?
You can sometimes reuse inks, but you almost never want exactly the same surface tension behavior. Jerseys are often sublimated polyester knits where ink must penetrate and bond inside the fiber, while banners and SEG graphics frequently rely on UV or latex films that sit more on the surface. Digital Output and Amayse both point to coatings and fabric engineering as critical for outdoor graphics: you need controlled stretch, stable dimensions, and surfaces tuned for the chosen ink set. In practice, shops that print both apparel and soft signage will either separate workflows or be very deliberate about fabric and coating choices to keep wetting behavior in the right zone for each application.
In performance sports and adventure gear, great digital printing is not an accident. It is the payoff of matching ink surface tension, fabric surface energy, construction, and coatings so everything works together under real‑world abuse. When you dial that in, your jerseys stay bright, your banners stay sharp, and your gear tells the story you want every time you roll out.
References
- https://www.cffaperformanceproducts.org/content/pdfs/SurfaceTension.pdf
- https://www.textiles.org/2007/01/01/selecting-the-right-ink-and-fabric-combination-for-digital-printing/
- https://digitaloutput.net/accessibility-to-the-textile-opportunity/
- https://www.researchgate.net/publication/272982227_Influence_of_paper_surface_characteristics_on_digital_printing_quality
- https://itacadhesives.co.uk/surface-coating-surface-tension-key-considerations-and-controls/
- https://www.exhibitoronline.com/topics/article.asp?ID=711
- https://www.gentlepk.com/digital-printing-on-fabric/
- https://www.gzhenrytextile.com/blog/choosing-the-right-fabric-for-digital-printing
- https://initibag.com/digital-printing-on-fabric/
- https://blog.luminite.com/blog/flexo-surface-tension-surface-energy-and-wettability
RELATED ARTICLES

Ready to start your sportswear brand?
Get a free quote for custom sportswear manufacturing with no minimum order quantity.